Solid Brass Watch Needles
Solid Brass Watch Needles
Clean Factory Solid Brass Watch Hands: Engineering & FinishingStandards
The hands of a mechanical watch are among its most precision-demanding moving components Operating with micro -clearances above the dialsurtace, watch hands must maintain rgid structural Integrity wthout adding unnecessary inertia to the movement cannon pinion Clean Factorymanufactures all hands using genuine solid bras stock-matching authentic material density, 3D dimensional profling, and muti-stageelectroplating rather than using cheap stamped aluminum. This technical guide ourtines our hand stamping, dioamond beveling, and uminous flingprotocols.
Hand Manufacturing Directory
1. Solid Brass Blank Stamping & Pinion Hole Punching
2. 3D Diamond Polishing & Side Chamfering
3. Rhodium & 18k Gold Galvanic Plating Protocols
4. Swiss Super-LumiNova Pigment Application
5. Technical Specification Matrix: Clean Hands vs. Cheap Alternatives
1. Solid Brass Blank Stamping & Pinion Hole Punching
Cheop replica actores often utkze thin stamped auminum or sort copper alloy for wctch hands, leodng to bending durg service and mproper friction ft onmovement pinions Clean Factory utlizes high-tensle solid brass strips.Precision progresive dies stamp out hour, minute, second, ond oMT hand profles whilesimuitoneously punching center mounting collars (annon pinion hales)to strict tolerances within 0.03mm. This precise fit ensures secure attochment to ourSuper Clone Movements without slipping over time.
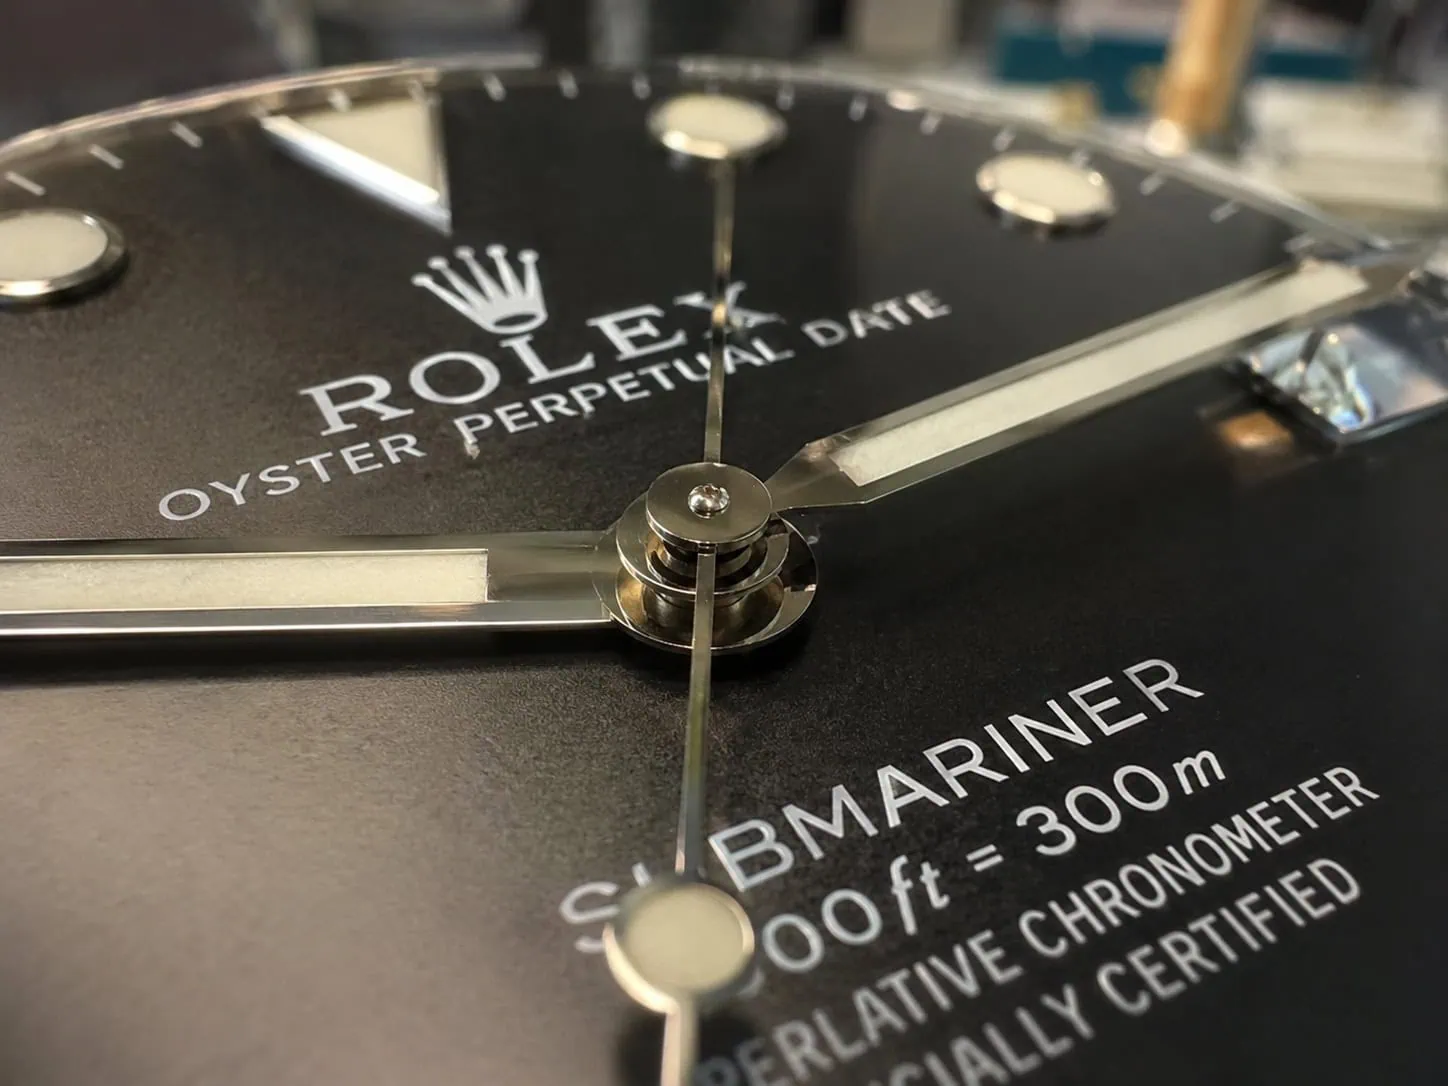
Figure I: Microscopic inspection verifying flat second hand rivet cap and cleancannon pinion hole clearance.
2. 3D Diamond Polishing & Side Chamfering
Flot lifeles watch hands immedictey betroy poor monufacturing under direct light Cean Factory subjects every bras hond blank to multi oxis diomondwheel polishing. This proces creates clean 3D top ridges and sharp lateral bevels angloge), alwing light to catch the edges sharply from any wrist angleParticular attention is given to the center hub cop, whichis polished flat to eliminate center-hole distortions typicalof mass-market replicas.
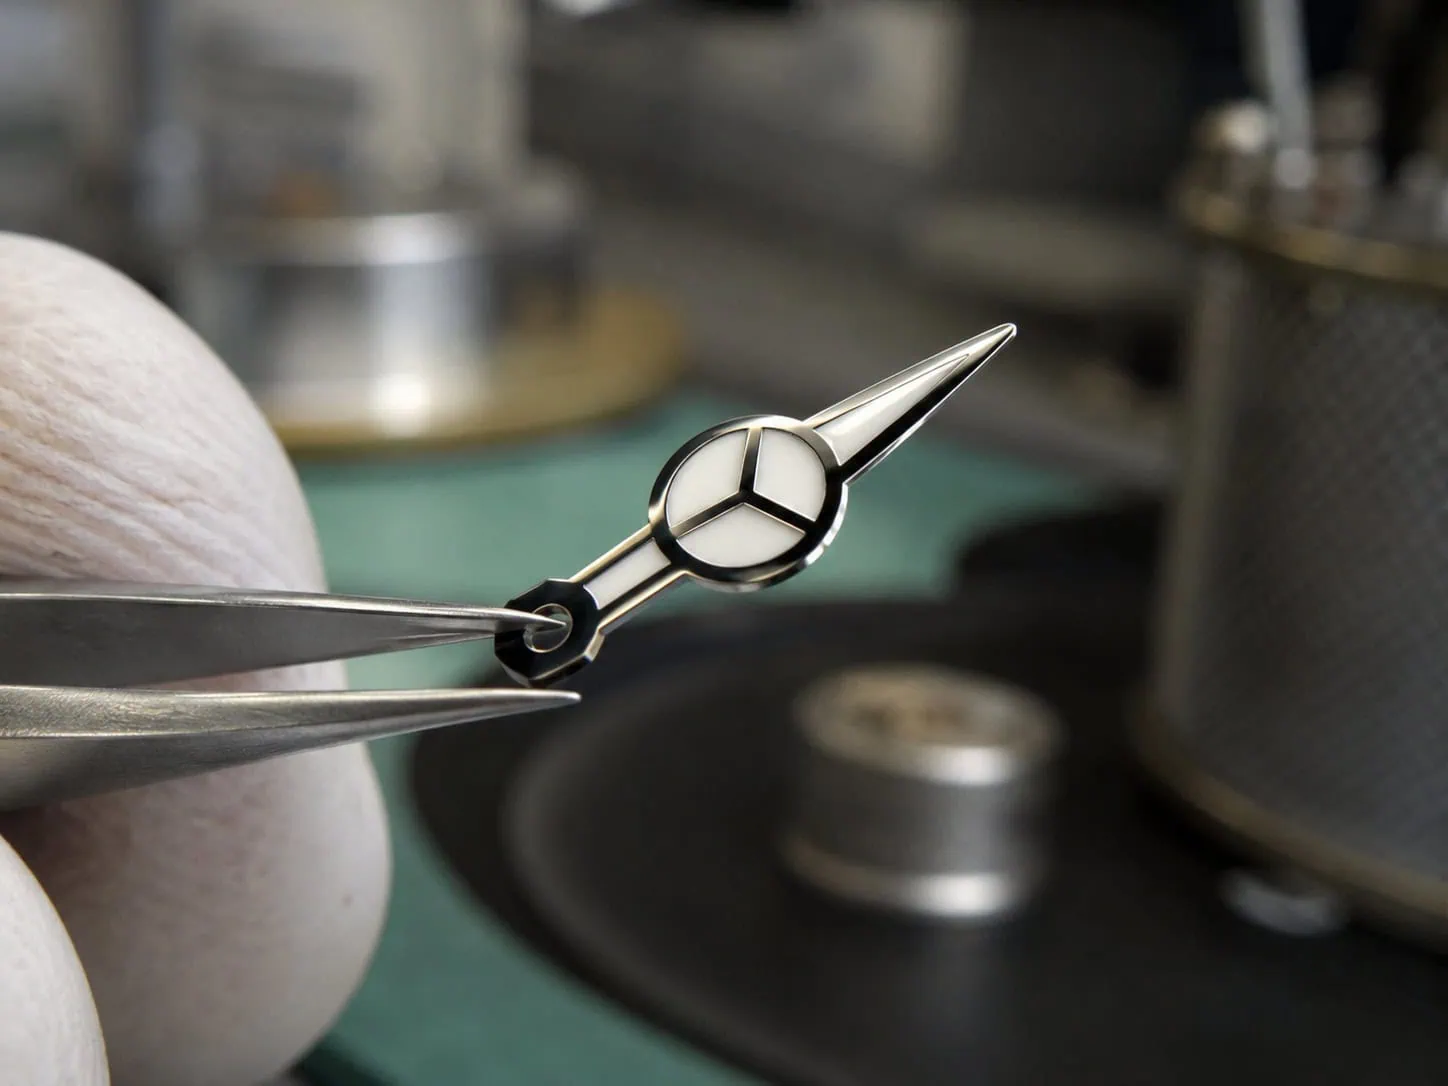
Figure 2: 45-degree angled view showing diamond-cut lateral bevels (anglage) onClean Factory solid brass hands.
3. Rhodium & 18k Gold Galvanic Plating Protocols
To achieve lasting metallic luster without tarnish or oxidation, polished hands undergo an extensive 6-stage galvanic bath treatment
ultrasonic Degreasing & Acid Pickling: Strips all residual polishing oils and microscopic surface oxides.
Nickel Undercoating: Seals the brass substrate and acts as a diffusion barrier.
Primary Galvanic Layer: Deposition of pure Rhodium (for steel references) or 18k Cold/Rose Cold (for two-tone references).
Deionized Water Rinsing: Prevents water-spotting or chemical staining during final hot-air drying.
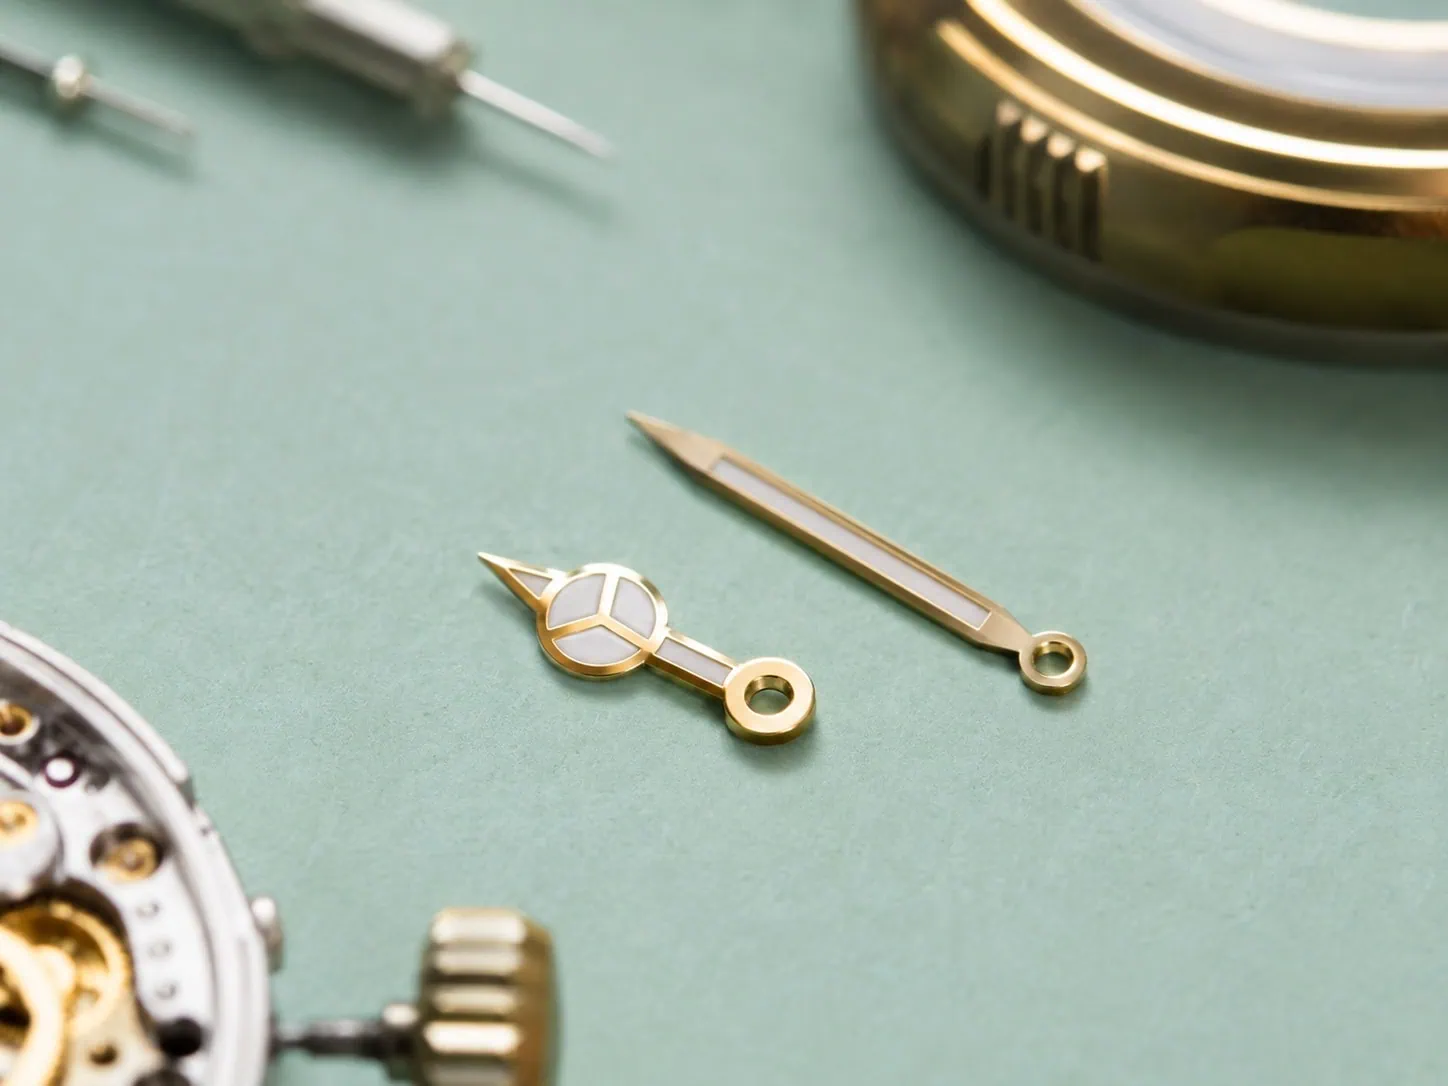
Figure 3: Inspection of 18k gold electroplated hands demonstrating tarnish-resistant surface uniformity.
4. Swiss Super-LumiNova Pigment Application
Luminous hands feature reverse -side micro-troughs designed to lock in luminous paste. Technicians apply outhenie Swiss Super-LumiNova (eGwsChromolight blue or C3 green)using pneumatic micrordispensers under stereoscopic microscopes. Copilary tension ensures the luminous compound spreodsevenly across the entire cutout area without sinking in the center or bleeding onto the electroplated metallic borders.
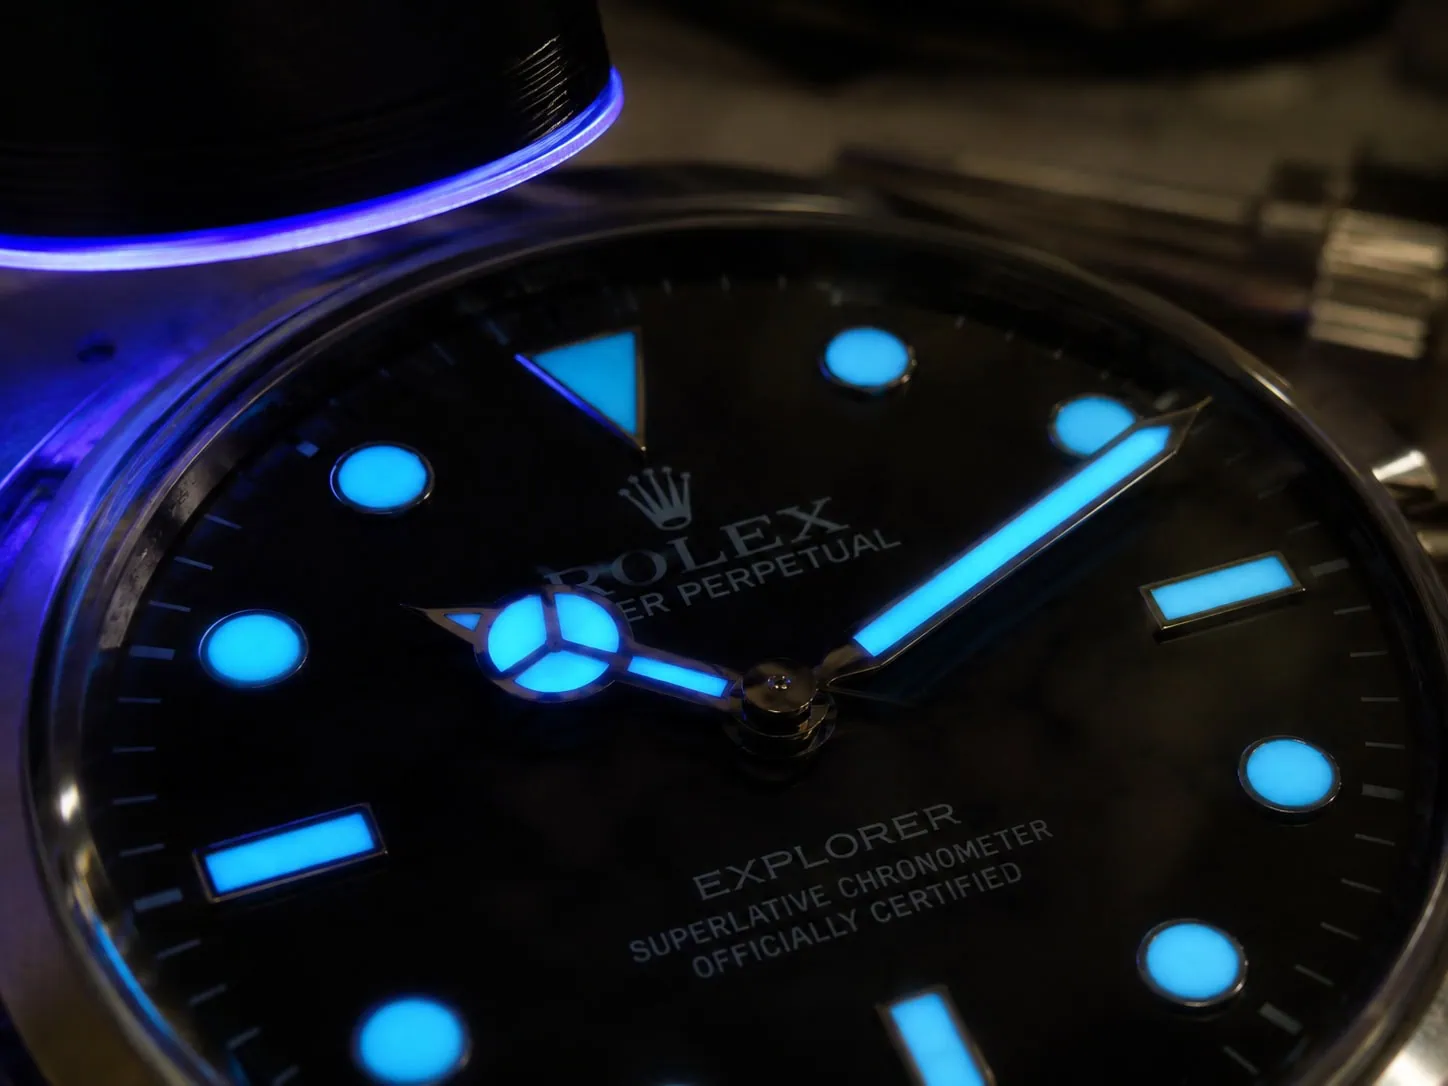
Figure 4: UV illumination test demonstrating uniform Chromalight blue glow intensity along hand cutouts.
Finished hand sets are paired with our custom Lacquered Dials and fitted into 904L Steel cases during Swiss Standard Assembly.