Lustrous Lacquered Dials
Lustrous Lacquered Dials
Clean Factory Watch Dial Craftsmanship: Lacquer, Sunray & AppliqueStandards
The watch dial serves as the primary visual intertace of any Luxury timepiece.Achieving true optcal party requires advanced metallurgical stamping.muti-loyer varnish depostion,and precise pad printing rather than simple surface sproying. Clean Factory manufactures custom watch dials onsolid bras substrates deploying specialized finishing techniques -including deep lacquering electroplated sunray brushing and femtosecond lasermotif engraving. This technical guide details our dial manufacturing workflow and quality verification metrics.
Dial Engineering Directory
1. Brass Substrate Milling & Surface Polishing Protocols
2. Multi-Layer Lacquering vs. Galvanic Sunray Electroplating
3. High-Precision Pad Printing & Thermal Oven Curing
4. Hand-Applied Hour Markers & Luminous Compound Filling
5. Technical Specification Matrix: Clean Dials vs. Standard Replicas
1. Brass Substrate Milling & Surface Polishing Protocols
and mountng e bocotons to talerontes wthin 00osmm. elre any oling ocours, the bionk disk unddrges mut- stags chemce deburing anddiamond-paste mirror polishing to eliminate surface imperfections.
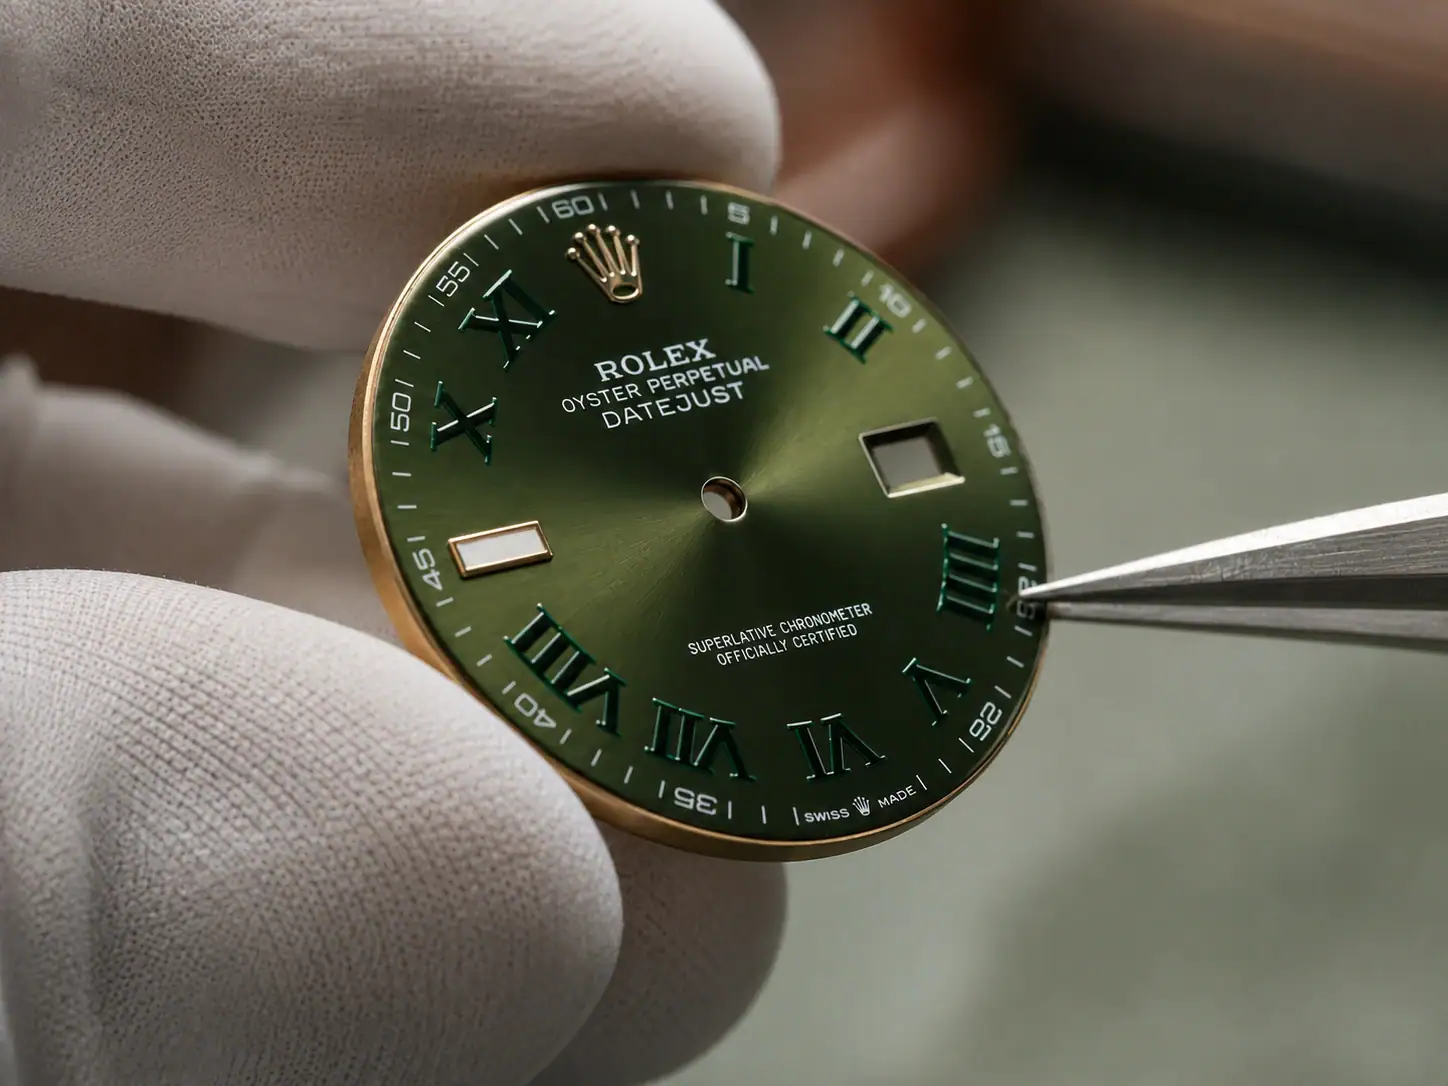
Figure t: Microscopic inspection of Clean Factory brass dial blank edge finishingand mirror polish
2. Multi-Layer Lacquering vs. Galvanic Sunray Electroplating
Different watch references require distinct surface metallurgy:
Gloss Lacquered Dials (e. g, Black submariner /White Daytona): Specialized acrylic varishes cre applied in cleanroom spray chambers Multiple ultra -thinlayers are baked in climate-controlled ovens, followed by clear-coat protective glazing to yield an enamel-like depth.
Galvanic Sunray Dials (e.g, Datejust Blue/reen): Bross banks are spun under brass-wire brushes to etch micro radialines. Disks are then immersed inelectrolytic baths containing gold, silver, or rhodium ions for dynamic reflection.
Laser Motif Dials (e.g. Palm& Futed Paterns): Femtosecond laser cutters carve precise geometric channels into the bros base before galvanic coloringproducing sharp visual contrast
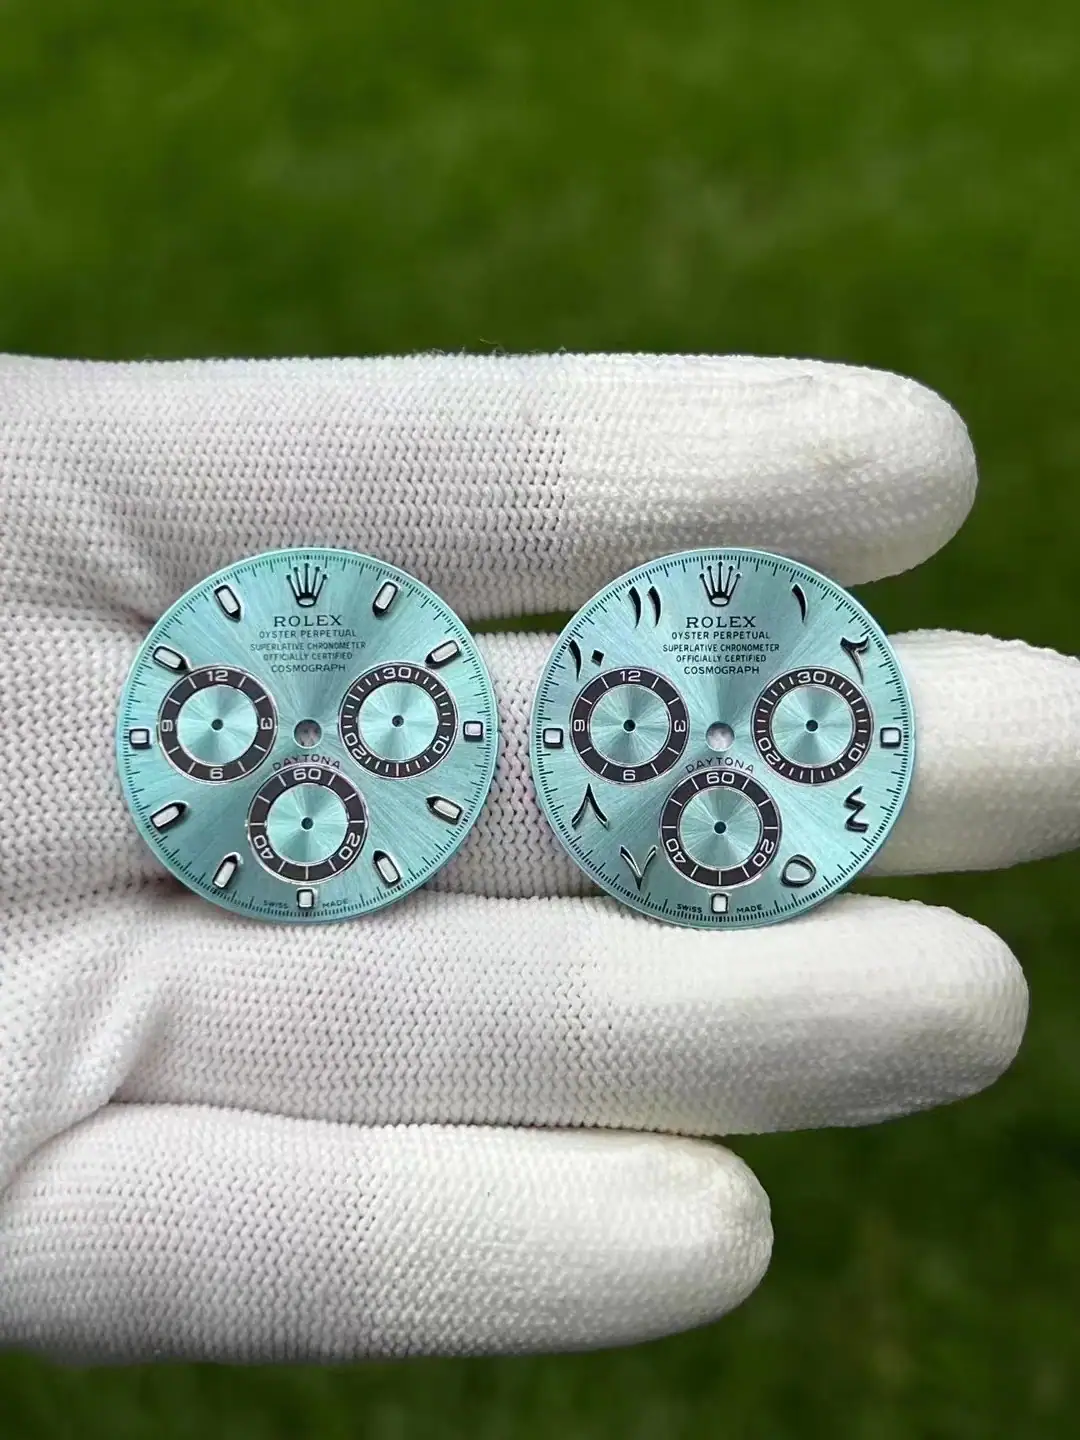
Figure 2: High-magnification check of Clean Factory sunray radial pattern and 3Dpad-printed text integrity.
3. High-Precision Pad Printing & Thermal Oven Curing
Inscriptions, minute tracks, and sub-dial indices are transferred using silicone transfer bulbs. Inks are custom-formulated for opacity and UV stability. To achieve crisp, 3D raised typography without ink bleeding, each color pass is printed separately and cured in thermal ovens at 120°C before subsequent passes.
4. Hand-Applied Hour Markers & Luminous Compound Filling
Hour-marker appliques (Roman numerals, batons, or geometric dots) are stamped from solid metal stock, diamond-cut along all bevels, and rhodium or 18k gold electroplated to prevent oxidation. Technicians manually position each marker using micro-tweezers under stereo microscopes, riveting them through rear dial feet.
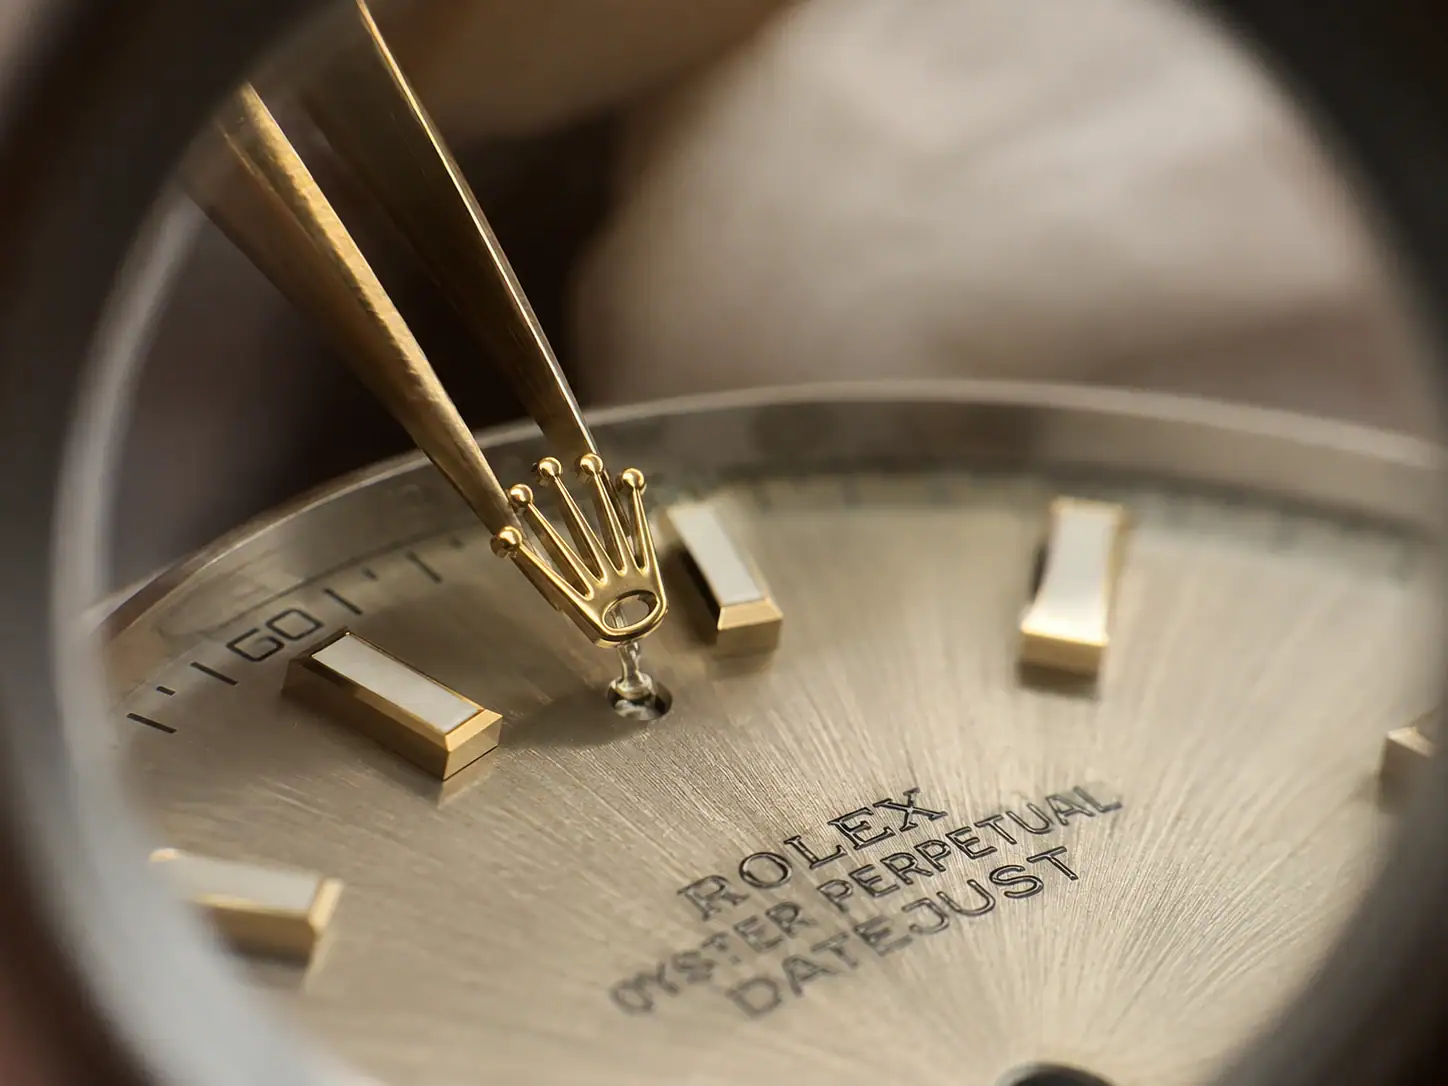
Figure 3: Benchwork precision setting of 1Bk gold plated appliques and Chromalightluminous fils.
Batons and hands -detoiled in our Solid Hands Guide -are flled with outhentic swiss Super-LumiNove pigments (Chromalight blue or C3 green). Completeddial assemblies are fitted to our g04L Steel cases during final Swiss-Standard Assembly.